16 bar Screw Air Compressors for Fibre Laser Cutting
A fibre laser cutter uses compressed air as its assist gas, and it needs that air at 10 to 16 bar, clean and dry, in bursts that follow the cutting cycle. Colt builds 16 bar VFD screw air compressors for exactly this job: 15 to 60 HP, 20 to 178 CFM at 16 bar, with an IE4 permanent magnet motor and a VFD that follows the laser's demand. Supplied with a refrigerated dryer and three-stage filtration, the air at the nozzle is virtually oil-free, so cut edges stay clean and the protective window lasts. Model table, sizing help and FAQs are below.
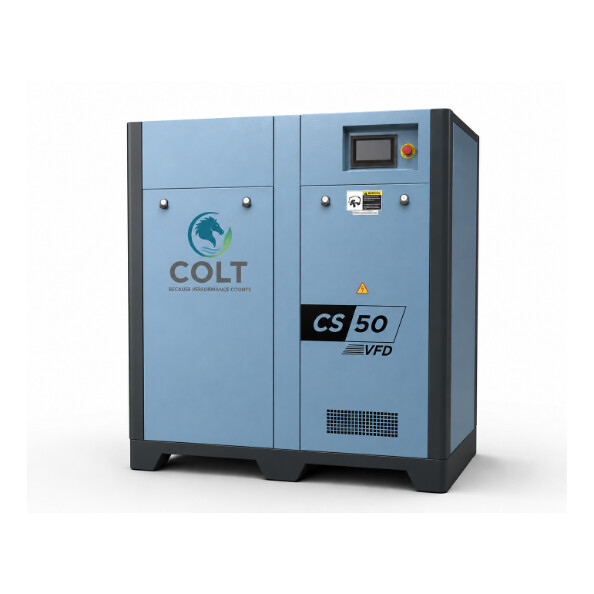
Laser-application screw compressor models (16 bar)
Free air delivery at 16 bar from our catalog. All models are VFD, 3 phase 400 V 50 Hz, IE4 permanent magnet motor, air cooled with oversized coolers for ambient temperatures up to 48 °C.
| Model | Motor (HP / kW) | FAD @ 16 bar (CFM) | Noise dB(A) | Size L×W×H (mm) | Outlet |
|---|---|---|---|---|---|
| CS 15 VFD | 15 / 11 | 20 – 38.3 | 70 | 1320×800×1320 | 1" |
| CS 20 VFD | 20 / 15 | 25.8 – 55 | 70 | 1320×800×1320 | 1" |
| CS 30 VFD | 30 / 22 | 53.1 – 71 | 70 | 1320×900×1500 | 1" |
| CS 40 VFD | 40 / 30 | 61.8 – 104 | 70 | 1500×1000×1450 | 1½" |
| CS 50 VFD | 50 / 37 | 70.3 – 139 | 70 | 1500×1000×1450 | 1½" |
| CS 60 VFD | 60 / 45 | 122 – 178 | 70 | 1500×1000×1450 | 1½" |
Larger models and other pressures are also available; ask us for their data sheets.
What a laser cutting air system needs
- 16 bar at the compressor. The nozzle needs 10 to 16 bar; the dryer, filters and piping take some of it, so the compressor is set to 16 bar.
- VFD. Demand jumps when the nozzle opens and falls while the sheet loads. The VFD follows it and holds the pressure steady, instead of a fixed-speed machine loading and unloading all day.
- Dry air. A refrigerated dryer as standard; a desiccant dryer (pressure dew point −40 °C) for stainless steel and aluminium, where any moisture shows on the edge.
- Three filters. Pre-filter, fine coalescing filter and activated-carbon filter, so no oil mist reaches the protective window.
- A receiver. 500 L for 15 to 30 HP, 1,000 L for 40 to 60 HP, to buffer the bursts.
Sizing: take the assist-air consumption from the laser maker's data sheet for your nozzle sizes and pressure, add about 20%, and match it to the FAD column above. Two lasers on one compressor: add their consumptions. Send us the laser model and we will size the package.
Related: all screw air compressors (8 to 13 bar) · fixed speed vs VFD · dryers, filters and receivers · air receiver sizing
Laser cutting air compressor FAQs
What air pressure does a fibre laser cutting machine need?
Most fibre laser cutters use compressed air as the assist gas at 10 to 16 bar at the nozzle. Allowing for the drop across the dryer, filters and piping, the compressor should deliver 16 bar. Colt's laser-application screw compressors are built for 16 bar as standard.
Why does the air have to be clean and dry?
Oil mist or moisture in the assist air burns onto the cut edge and fogs the protective window and lens, so cut quality drops and consumables wear faster. A laser line needs a refrigerated dryer, a pre-filter, a fine coalescing filter and an activated-carbon filter after the compressor; for stainless steel and aluminium, a desiccant dryer gives the driest air.
Are these compressors oil-free?
They are oil-injected screw compressors. With the dryer and three-stage filtration above, the air at the nozzle is virtually oil-free and well within what laser makers specify. If the machine builder insists on an oil-free compressor, ask us; we also build oil-free reciprocating machines.
Why VFD for a laser?
A laser cuts in bursts: air demand jumps when the nozzle opens and falls while the sheet is loaded or the head repositions. A VFD compressor follows that pattern, holds a steady pressure and avoids the energy loss of a fixed-speed machine unloading and reloading all day.
How do I pick the size?
Take the assist-air consumption from the laser maker's data sheet for your nozzle size and pressure, add about 20% for leaks and future nozzles, and match it to the FAD at 16 bar in the table. If you run two lasers from one compressor, add their consumptions. Send us the laser model and nozzle sizes and we will size it for you.
What else goes in the package?
A vertical air receiver (500 L for 15 to 30 HP, 1,000 L for 40 to 60 HP), the dryer, the filter set and a high-pressure piping run to the laser. Colt supplies and commissions the complete system.
SEND YOUR LASER MODEL FOR A QUOTE
Model data from the Colt combined catalog. Last updated: .